Book Appointment Now
PCB laminate quality is decided long before drilling: how to read a datasheet, what to check on arrival, and which tests actually predict field failures.
PCB Laminate Quality: How to Inspect Incoming Material
PCB laminate quality is settled before the first hole is drilled, and it is settled with paperwork as much as with instruments. A board can pass every electrical test on the line and still fail in the field because the laminate under it was not the grade that was ordered, was pressed from a lot with a low decomposition temperature, or absorbed moisture in storage. The failure appears months later as measling, delamination or a cracked barrel, at which point nobody can trace it back to the material.
This guide is written from the receiving-inspection side of that problem. It covers what a datasheet should state and what those numbers predict, the visual and dimensional checks worth doing on arrival, the thermal, CTE, electrical and chemical tests that change a decision, and the sampling and record-keeping that make a failed lot a contained event instead of a batch scrap. Nothing here requires a fully equipped laboratory — most of it is a checklist and a set of questions.
Table of Contents
- Why PCB Laminate Quality Is Settled Before the First Drill
- What a PCB Laminate Quality Datasheet Should Tell You
- Visual and Dimensional Checks on the Receiving Dock
- Thermal Limits in Practice: Tg, Td and T260/T288
- Z-Axis CTE and What It Predicts About Plated Holes
- Dk, Df and Resistivity: When These Numbers Change a Decision
- Peel Strength, Flexural Strength and Handling Damage
- Chemical Checks That Affect PCB Laminate Quality
- Sampling Plans, Records and What to Do With a Failed Lot
- Storage, Moisture and What Happens Before Press
- FAQ
- Ask for the Material Specification Before the First Panel
Why PCB Laminate Quality Is Settled Before the First Drill
Copper clad laminate is the single largest material input by area in a PCB shop, and it is the one with the least visible evidence of being wrong — which is why PCB laminate quality has to be verified rather than assumed. A wrong copper weight shows up on a cross-section; a wrong resin system shows up as delamination after reflow, or as a plated barrel that cracks after two hundred thermal cycles. By then the panel is scrap and the cause is two process steps and three weeks behind you.
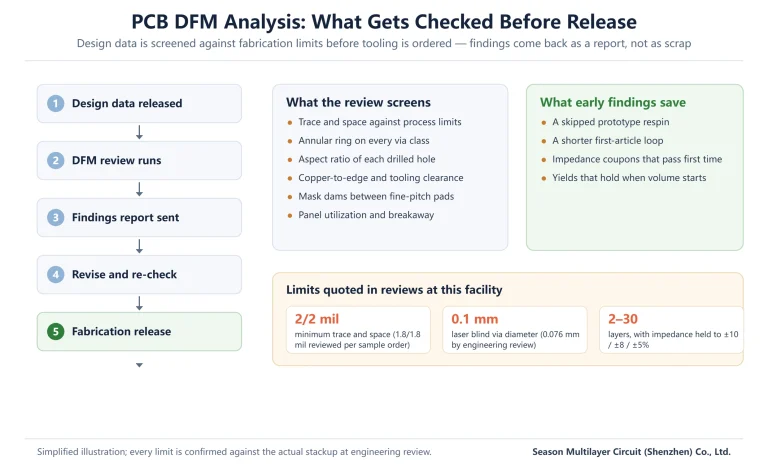
Incoming inspection is therefore not a bureaucratic step, it is the cheapest control point in the whole flow. Catching a substituted grade at the dock costs a phone call. Catching it after lamination costs the whole panel, plus the drilling and imaging time already invested, plus the schedule. The point of a checklist is to make that catch routine rather than dependent on somebody noticing something odd.
There is also a procurement angle. Laminate is bought to a grade, and grades with similar headline numbers are not interchangeable — a Tg figure alone tells you nothing about decomposition temperature, z-axis expansion or tracking resistance. Writing those numbers onto the purchase specification, and requiring them on the lot certificate, is what turns a material claim into something you can verify.
What a PCB Laminate Quality Datasheet Should Tell You
A usable datasheet gives three things for every property: the test method, the test condition and a typical value. Without the method the number cannot be compared; without the condition it cannot be reproduced. The table below is the structure we expect to see for an FR-4 class material, with representative values from a high-Tg grade — the same property set applies whether the ordered material is a mid-Tg, Tg 170/180 or halogen-free product. For the selection side of the same decision, our laminate selection guide covers how these grades map onto design intent.
| Property | Test method | Condition | Typical value (Tg 180 FR-4) | What it predicts |
|---|---|---|---|---|
| Tg | IPC-TM-650 2.4.24.4 / 2.4.25D | DMA / DSC | 185 °C / 180 °C | Where expansion and modulus change |
| Td | IPC-TM-650 2.4.24.6 | TGA, 5% weight loss | 355 °C | Reflow and rework headroom |
| T260 / T288 / T300 | IPC-TM-650 2.4.24.1 | TMA | >60 min / 30 min / 15 min | Delamination resistance in assembly |
| Thermal stress | IPC-TM-650 2.4.13.1 | 288 °C solder dip | >100 s | Resin integrity at solder temperature |
| CTE, z-axis | IPC-TM-650 2.4.24 | Before / after Tg | 41 / 208 ppm/°C | Strain on plated hole barrels |
| CTE, z-axis total | IPC-TM-650 2.4.24 | 50–260 °C | 2.4% | Cumulative expansion over a cycle |
| Dk / Df | IPC-TM-650 2.5.5.9 | 1 GHz, C-24/23/50 | 4.6 / 0.018 | Impedance and insertion loss |
| Volume / surface resistivity | IPC-TM-650 2.5.17.1 | C-96/35/90 | 8.7 × 10⁸ MΩ·cm / 2.2 × 10⁷ MΩ | Insulation reliability after humidity |
| Dielectric breakdown | IPC-TM-650 2.5.6 | D-48/50 + D-0.5/23 | >45 kV | Withstand margin at high voltage |
| Peel strength | IPC-TM-650 2.4.8 | 1 oz, 288 °C / 10 s | 1.3 N/mm (7.43 lb/in) | Foil adhesion through thermal stress |
| Flexural strength | IPC-TM-650 2.4.4 | Lengthwise / crosswise | 567 / 442 MPa | Handling and mechanical margin |
| Water absorption | IPC-TM-650 2.6.2.1 | D-24/23 | 0.08% | Drying requirement before press |
| Flammability | UL 94 | C-48/23/50 | V-0 | Finished-board safety recognition |
| CTI | IEC 60112 | Method A | PLC 3 | Creepage distance for high voltage |
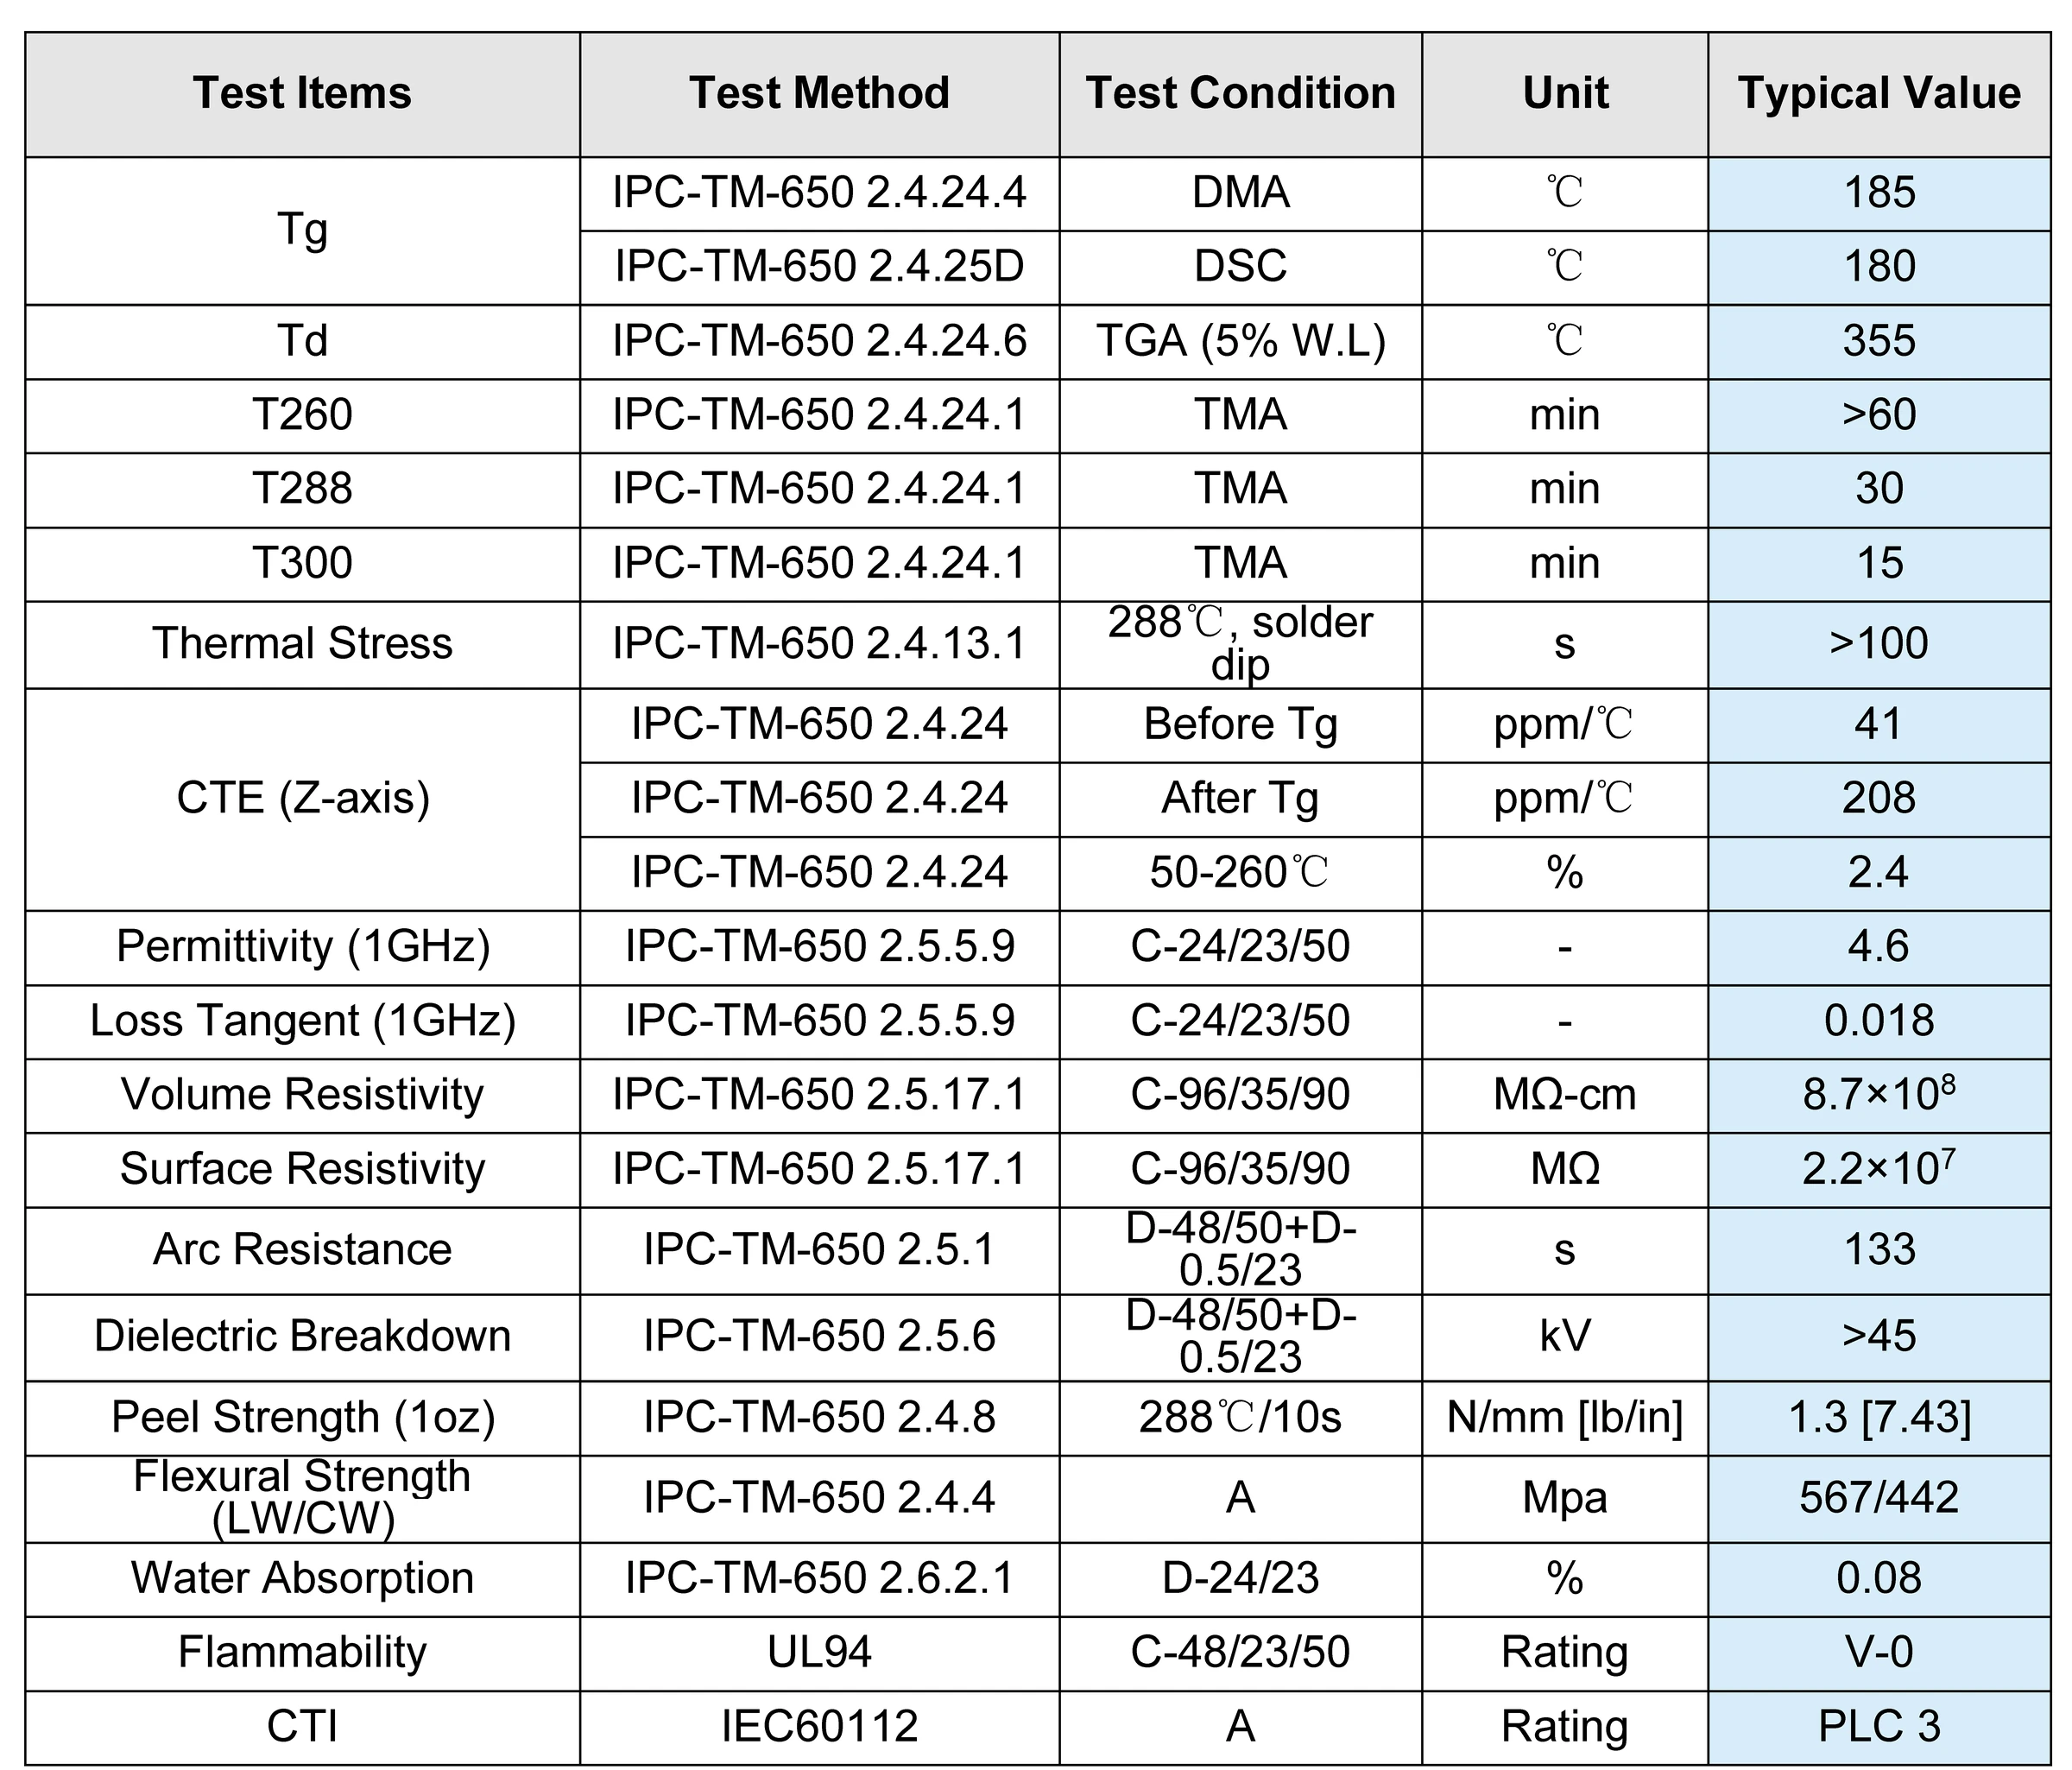
Two columns in that table get ignored most often. The method column matters because DSC and DMA Tg readings on the same sheet differ by roughly 5 °C, so a supplier quoting one method against another’s number can look better or worse for no material reason. The condition column matters because properties such as peel strength and breakdown voltage are meaningless without the thermal or humidity conditioning that preceded them.
If a datasheet arrives with a single Tg number, no method and no CTE figures, that is not a data sheet, it is a brochure. Ask for the full property table before the material is approved, because the numbers you cannot get at the approval stage are the ones you will not get during a dispute.
Visual and Dimensional Checks on the Receiving Dock
Visual inspection catches a surprising share of PCB laminate quality problems, and it costs minutes per lot. Work on a clean bench under even light, look at both faces of every sheet in the sample, and check the edges as well as the surface. Defects that matter are the ones that survive into the finished board: inclusions and foreign particles become opens or shorts, resin starvation becomes delamination, and edge damage becomes handling scrap.
| Check | What to look for | What it usually indicates | Action |
|---|---|---|---|
| Surface cleanliness | Particles, stains, fingerprints, resin spots | Handling or storage damage, dirty sheeting | Reject affected sheets; review storage practice |
| Foil appearance | Scratches, oxide discolouration, dents | Transport damage, oxidation from poor packing | Reject; check the rest of the shipment |
| Thickness uniformity | Thickness measured at multiple points per sheet | Press control problem at the laminate maker | Reject if outside the ordered tolerance |
| Flatness | Bow and twist against a straight edge | Asymmetric build or wrong cooling cycle | Segregate; bow affects registration and handling |
| Edge quality | Chipping, burrs, delamination at the cut edge | Dull cutting tools, moisture pickup | Trim before use or reject |
| Visible weave / resin | Resin starvation, exposed glass, dry spots | Resin content below specification | Reject — a known delamination precursor |
| Marking and identity | Grade, lot, date, thickness, copper weight | Wrong material or mixed lots in one carton | Stop and reconcile against the purchase order |
The last row is the one that catches substituted material, which is the failure mode with the largest consequences. Every carton should carry grade, lot number, build date, nominal thickness and copper weight, and those fields should match the purchase order and the certificate. When a carton is unmarked or the markings disagree, the correct response is to quarantine rather than to use it on a non-critical order — mixed lots are how a traceability system quietly stops working.
Dimensional checks are simple and worth doing properly: thickness at several points per sheet, copper weight confirmed against the ordered value, and panel dimensions against the tooling you will use. A laminate that is 0.05 mm thin will move the finished board thickness out of tolerance and will change the impedance of every controlled line on the design, which is a problem you do not want to discover at final inspection.
Thermal Limits in Practice: Tg, Td and T260/T288
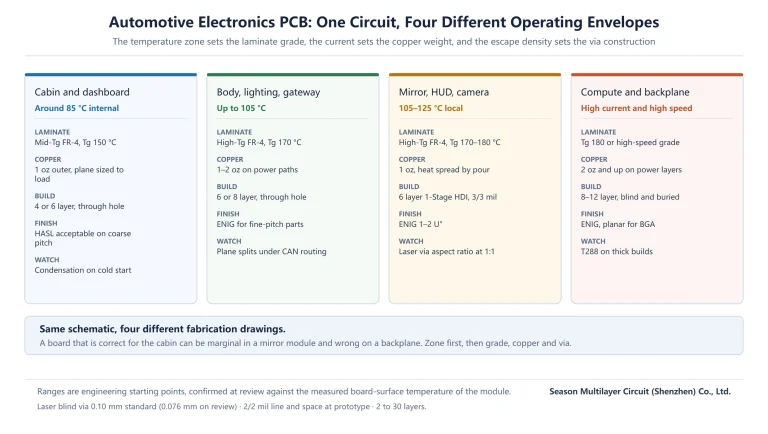
Tg is the number everybody quotes and the one most often misunderstood. It marks the transition where the resin softens, the z-axis expansion rate multiplies and the modulus drops. It is not a maximum service temperature: a Tg 150 material still functions well above 150 °C, but the mechanical behaviour there is different, and every plated hole in the board is being asked to absorb that difference on each thermal cycle.
Td and the T260/T288 pair describe what happens when the material is pushed rather than used. Decomposition temperature is measured by thermogravimetric analysis at 5% weight loss and typically sits near 355 °C on a Tg 180 FR-4 grade — comfortably above lead-free reflow peaks, which is why reflow alone rarely destroys a correct laminate. Time-to-delamination at 260 °C and 288 °C is the more discriminating test for thick boards and heavy copper, because those builds hold heat longer and see more cumulative exposure during assembly and rework.
If you can only run one thermal verification on an incoming lot, run the solder-dip thermal stress test at 288 °C and inspect the sample for measling and blistering. It is fast, it needs no exotic equipment, and it catches the failures that matter: moisture pickup, under-cured resin and a grade that is not what the certificate claims. Verification of CTI and tracking behaviour belongs to the electrical side of the checklist and is covered in our CTI ratings guide; the reference method is IEC 60112.
Z-Axis CTE and What It Predicts About Plated Holes
The z-axis coefficient of thermal expansion is where PCB laminate quality meets field reliability, because it is the property that connects a datasheet to a cracked barrel. Below Tg the expansion is modest — around 41 ppm/°C on the grade in the table above. Above Tg it jumps to roughly 208 ppm/°C, and the total expansion from 50 °C to 260 °C lands near 2.4%. That total figure is what a plated barrel has to survive in elongation, cycle after cycle, while the copper itself wants to stay where it is.
This is why board thickness and hole diameter are reliability variables, not just layout variables. A short hole in a thin board accumulates less absolute strain than a long hole in a thick one, and a barrel with uniform plating distributes that strain better than one with thin spots. It is also why the laminate grade and the aspect ratio have to be decided together: moving to a higher Tg grade reduces expansion above the transition, but only if the hole is drilled and plated to match. The drilling and plating limits are set out in our aspect ratio guide, and the same mechanics sit behind our drilling process comparison.
For incoming verification, a CTE figure on the lot certificate is usually accepted on the strength of the material grade rather than re-measured — thermomechanical analysis is not a dock instrument. The practical control is therefore identity control: confirm the grade, then rely on the grade’s published CTE. Where a program needs more assurance, ask for the laminate maker’s batch test report rather than attempting to replicate it in-house.
Dk, Df and Resistivity: When These Numbers Change a Decision
Dielectric constant and dissipation factor decide impedance and loss, so on any controlled-impedance design they are a direct expression of PCB laminate quality rather than background information. A standard FR-4 class material sits near Dk 4.6 and Df 0.018 at 1 GHz. That is entirely adequate for control and power boards, and increasingly marginal for multi-gigabit interfaces, which is why high-speed designs move to lower-Dk materials rather than compensating with wider lines.
The verification question for incoming material is not whether the Dk is exactly 4.6 — it varies with resin content and with the glass style in the sheet — but whether it is inside the window the design assumed. If impedance is held to ±10% this tolerance is generous; at ±5% it is tight enough that laminate variation alone can consume it. How that variation is measured and controlled on coupons is covered in our impedance measurement guide.
Resistivity figures look impressive on paper and are mostly a check on cleanliness and cure rather than a design input. A volume resistivity reading in the 10⁸ MΩ·cm range after humidity conditioning tells you the resin is properly cured and the sheet is not contaminated. When a lot fails insulation resistance on finished boards, resistivity and ionic contamination are the two material-side explanations worth checking before blaming the plating line.
Peel Strength, Flexural Strength and Handling Damage
Of all the numbers on the datasheet, peel strength reflects PCB laminate quality most directly, because it measures foil-to-resin adhesion and it degrades first when a sheet has been stored badly or cured incorrectly. On a 1 oz foil, a value around 1.3 N/mm measured after a 288 °C solder dip is typical for a good FR-4. A reading well below that on an incoming sample is a warning about the material, not about the process.
Flexural strength sits in the background until something goes wrong in handling or in a thin, large-format board. Lengthwise and crosswise values differ because the glass weave is directional, and a board that is noticeably weaker in one direction will show it as cracking along a panel edge or at a connector cut-out. On thin builds, this is one of the arguments for keeping panel utilisation and support tooling under control rather than pushing both.
Handling damage is the practical form of all of this. Sheets stacked on edge, dragged across a bench or stored without interleaving pick up scratches, dents and edge chips that become etch defects. A laminate store with flat shelving, interleaved sheets, controlled humidity and a first-in-first-out rule removes a whole category of scrap before it exists.
Chemical Checks That Affect PCB Laminate Quality
Chemical verification answers the questions identity control cannot, and it is the part of PCB laminate quality that a certificate alone cannot prove: is this really the resin system claimed, is it free of the substances the program restricts, and is it clean enough for the insulation requirements of the design. You do not need a full laboratory to act on the answers — you need a supplier who can provide the reports, plus a sampling policy that checks them occasionally against reality.
Halogen content is the most common procurement-driven check. Brominated FR-4 grades are standard and entirely legitimate; a halogen-free program simply requires a different grade, and the only way to prove the substitution happened is a composition test. X-ray fluorescence gives a fast elemental screen for bromine and for the restricted heavy metals, which is why it is the usual first pass on both halogen verification and RoHS declarations. Note that XRF screens elements, not compounds — for a formal declaration, the supplier’s test report carries the weight.
Ionic contamination and resin content are the two internal checks worth running periodically. Ionic contamination shows up later as electrochemical migration and insulation resistance drift, and it is usually a wet-process problem rather than a material problem — but it starts with what is on the incoming sheet. Resin content below specification produces resin-starved areas, which is a direct precursor to delamination and measling. Infrared spectroscopy identifies the resin system quickly when a grade is in doubt, and it is the practical way to prove that two cartons of the same nominal grade are actually the same material.
Flammability recognition closes the chemical section. A V-0 rating to UL 94 belongs to the material and to the construction that was tested, so a laminate substitution changes the recognition. If your finished board carries a UL 796 file, the laminate grade on the certificate must match the grade in the press — that is a documentary check, and it is one of the cheapest ones available.
Sampling Plans, Records and What to Do With a Failed Lot
Sampling is where most inspection systems quietly fail, not because the tests are wrong but because the sample is not representative. Draw from more than one position in the carton, from more than one carton where the shipment allows it, and from throughout the stack rather than the top three sheets. A lot that looks uniform at the top of a carton can be a mixed pallet underneath.
| Check | Frequency | Sample | Record to keep |
|---|---|---|---|
| Identity and marking | Every carton | All cartons | Grade, lot, date, thickness, copper weight against the purchase order |
| Visual and dimensional | Every lot | Several sheets per carton, both faces | Thickness readings, defect photos, accept / reject decision |
| Solder-dip thermal stress | Every lot or per agreed skip-lot plan | One coupon set per lot | Conditioning, temperature, result, inspection notes |
| Peel strength | Per lot on new grade, then periodic | One coupon set | Foil weight, condition, measured value, method |
| Composition and halogen screen | Per supplier per grade, then periodic | One sample | Method, element screen result, supplier declaration reference |
| Full property review | On grade change or supplier change | Supplier report | Complete datasheet with methods, filed against the part number |
A failed lot needs a written path, decided before it happens. Quarantine the cartons, hold the certificate and the shipping documents, notify the supplier with the lot number and the measured deviation, and do not release the material into production on a verbal assurance. If the failure is identity-related — wrong grade, mixed lots, missing markings — treat the whole shipment as suspect rather than the sample, because the defect is in the supplier’s control system rather than in one sheet.
Records are what turn individual inspections into a trend. Three numbers are worth plotting: incoming defects by supplier, thermal stress failures by lot, and insulation resistance failures traced back to a material lot. When one of those lines starts to move, the cause is usually visible before a customer sees it. Acceptance criteria for the completed board belong to a different document — IPC Class 3 acceptance defines what the finished article must satisfy, while incoming inspection protects the process that produces it.
Storage, Moisture and What Happens Before Press
Moisture is the quietest PCB laminate quality variable: water absorption around 0.08% sounds trivial until it is converted into what happens at 288 °C. Absorbed moisture flashes to steam during solder dip or reflow, and the resulting pressure delaminates the resin or blisters the surface. That is why the thermal stress test is meaningful only if the sample has been conditioned, and why storage conditions are part of laminate quality rather than an afterthought.
The practical controls are unglamorous. Store in a dry, temperature-stable area with sheets flat and interleaved, keep cartons sealed until use, respect the material’s shelf life, and bake where the grade and the storage history call for it. Sheeted prepreg is far more sensitive than cured laminate and should follow the supplier’s stated out-time rules rather than a general habit.
- Flat shelving with interleaved sheets; never store laminate on edge
- Sealed cartons opened only at the point of use, first in first out by lot date
- Humidity and temperature logged in the store, with a defined action level
- Bake decision recorded per lot where storage history or the grade requires it
- Prepreg out-time tracked against the supplier’s stated limit, not a workshop rule of thumb
Incoming inspection and storage control are two halves of the same argument: the material has to arrive as specified and stay that way until it is pressed. Our own material policy and the laminate families we hold in stock are set out under PCB materials and laminates, and the inspection regime behind it is part of the process described on the manufacturing capability page.
Frequently Asked Questions
How do I check PCB laminate quality on arrival?
Start with identity: grade, lot, build date, thickness and copper weight on every carton, matched against the purchase order and the certificate. Then run visual and dimensional checks on several sheets per carton, both faces and edges, followed by a 288 °C solder-dip thermal stress test on a coupon set and inspection for measling or blistering.
What does Tg actually tell me about a laminate?
Tg marks the glass transition, where the resin softens, modulus drops and z-axis expansion multiplies from roughly 40–50 ppm/°C to around 200 ppm/°C. It is not a maximum working temperature. Always compare Tg values measured by the same method, because DSC and DMA readings on the same material differ by about 5 °C.
Why do T260 and T288 matter more than Tg for thick boards?
Because they measure time to delamination at a fixed elevated temperature, which is what thick boards and heavy copper actually experience during assembly and rework. Requiring T288 of at least 30 minutes and T260 above 60 minutes screens out laminates that survive a datasheet check but blister after a second reflow.
Can I verify halogen-free material with X-ray fluorescence?
XRF gives a fast elemental screen and is the usual first pass for bromine, but it screens elements rather than compounds. For a formal halogen-free declaration you need the supplier’s test report and a periodic composition check against it. A halogen-free program should also specify the grade explicitly, since brominated FR-4 remains the standard product.
What is a normal peel strength for FR-4?
Around 1.3 N/mm (roughly 7.4 lb/in) on 1 oz foil measured after a 288 °C solder dip is typical of a good FR-4. Much lower values on an incoming sample point to poor adhesion, under-cure or storage damage, and should trigger a hold rather than a release into production.
How does laminate quality affect impedance?
Dielectric constant sets the impedance of every controlled line, and it varies with resin content and glass style. A standard FR-4 class material sits near Dk 4.6 at 1 GHz. At ±10% impedance tolerance this variation is comfortable; at ±5% it consumes a large part of the budget, which is why coupon measurement and lot consistency matter on high-speed designs.
What should happen when an incoming laminate lot fails inspection?
Quarantine the cartons, hold the certificate and shipping documents, and notify the supplier with the lot number and the measured deviation in writing. If the failure involves identity — wrong grade, mixed lots or missing markings — treat the entire shipment as suspect, because the defect sits in the supplier’s control system rather than in one sheet.
Ask for the Material Specification Before the First Panel
If you are qualifying a new build, send the stackup and the properties that matter for your application. We will return the laminate grade we would press, the property table for it with test methods stated, and the incoming inspection items we apply to that grade — so the material question is closed before the first panel is cut.
Material and process questions run through our PCB manufacturing services, covering 2 to 30 layers, mid-Tg and Tg 170/180 FR-4 grades, halogen-free grades, high-speed laminates and 1-Stage through Any-layer HDI. Where a program requires traceability per lot, say so at quotation so the documentation chain is set up with the order.